ADVANCED ZLD TECHNOLOGY

ZERO LIQUIDDISCHARGEWATER HARVESTER

Revolutionary humidification-dehumidification technology that transforms industrial wastewater into valuable resources through precision engineering and nature-inspired processes.

99%
WATER RECOVERY
60-90°C
OPERATION TEMP
ZERO
DISCHARGE
VIEW TECHNICAL SPECS
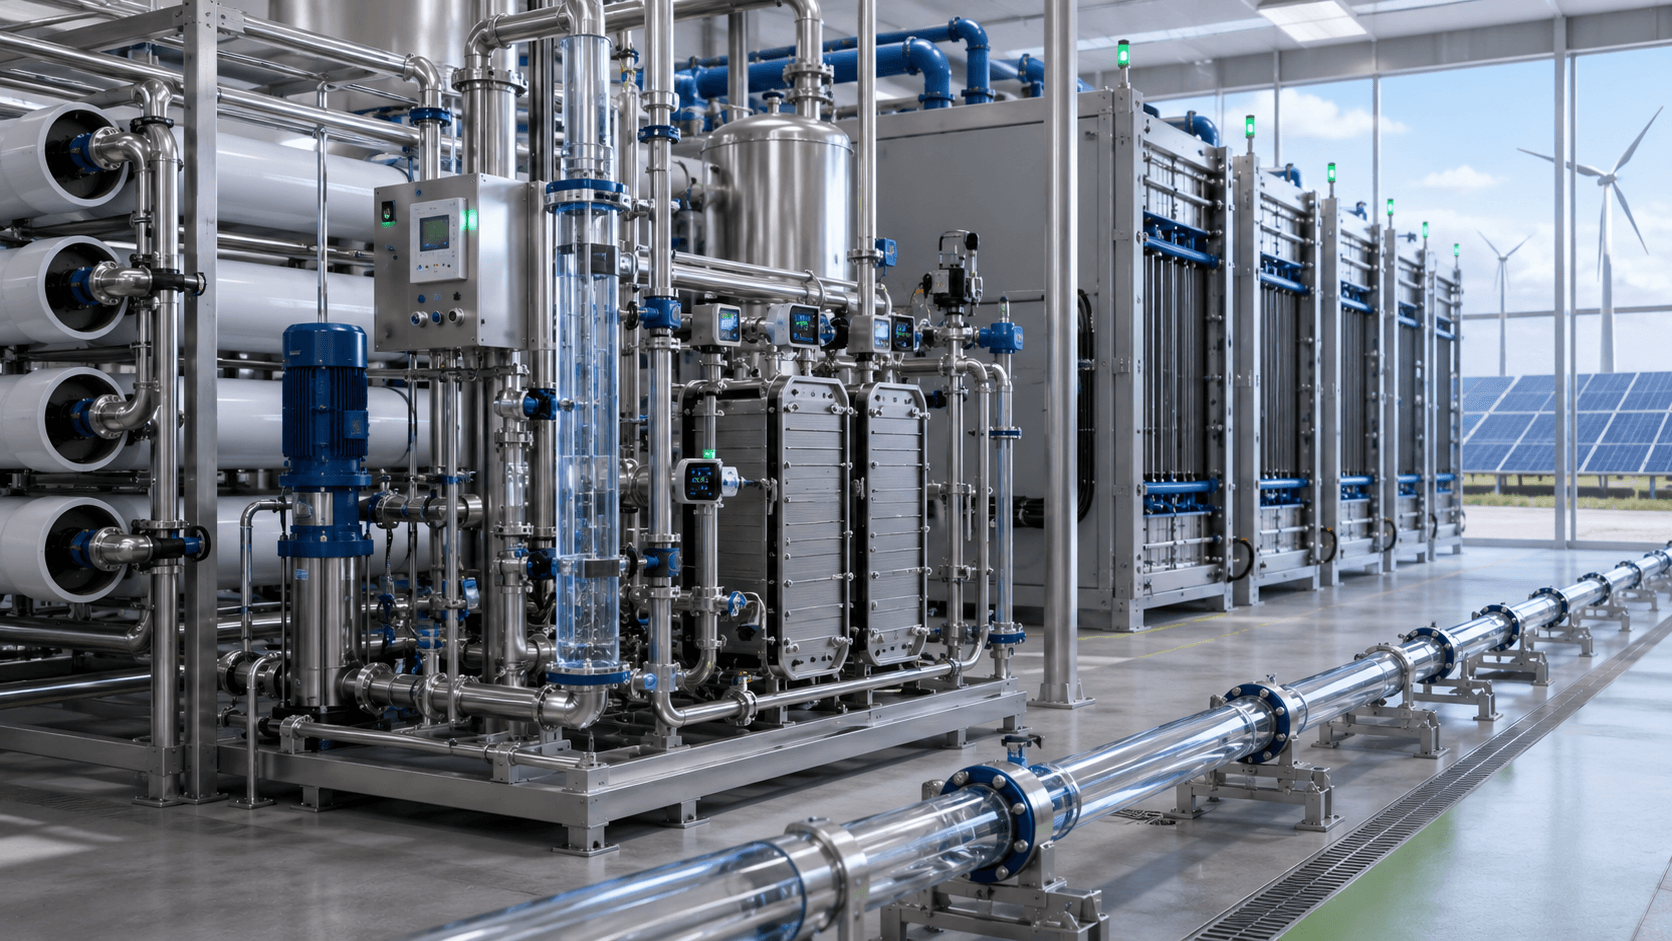
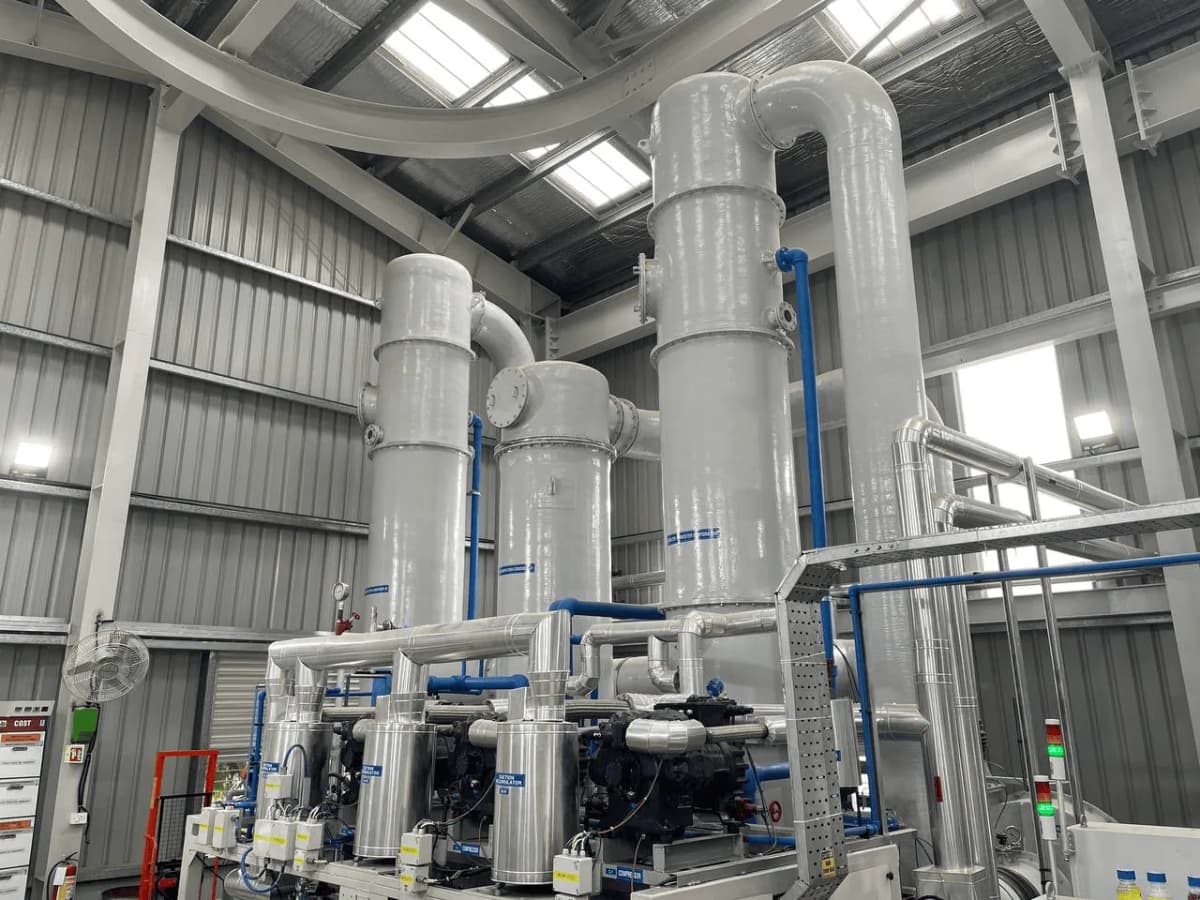
Zero Liquid Discharge Water Harvester industrial wastewater treatment system - 99% water recovery technology by Ionic Engineering

SYSTEM SPECIFICATIONS

Precision-engineered parameters for optimal performance

RECOVERY RATE

99%

Maximum water recovery through advanced HDH process

OPERATING TEMP

60-90°C

Low-temperature operation reduces energy consumption

ENERGY EFFICIENCY

60% SAVINGS

Compared to traditional MEE systems

PRESSURE

AMBIENT

No vacuum pumps required - ambient pressure operation

SYSTEM ARCHITECTURE

Core Components:

  • FRP Construction with Vinyl Ester Resin
  • Multi-Step Heat Recovery System
  • Automated Clean-in-Place (CIP) System
  • IoT-Enabled Monitoring & Control
  • Heat Pump Recycling Unit

Safety Features:

  • Automated Interlocks & Sensors
  • Drum Lifting & Tilting Mechanisms
  • Corrosion-Resistant Materials
  • Remote Monitoring Capability
  • Emergency Shutdown Systems

PROCESS FLOW DIAGRAM

Five-Step humidification-dehumidification cycle

01

HUMIDIFICATION

Wastewater evaporation using saturated steam at 6 bar pressure

02

ENERGY RECOVERY

Heat exchangers and heat pump recycling preheat incoming wastewater

03

DEHUMIDIFICATION

Hot vapor condensation through advanced heat recovery systems

04

CONCENTRATION

Drum evaporator processes concentrated salts into manageable slurry

05

POST-TREATMENT

Water polishing through filter media and cartridge systems

TECHNICAL ADVANTAGES

vs Traditional MEE Systems:

Energy Efficiency: 60% reduction in power consumption
Material Costs: Non-metallic construction eliminates expensive alloys
Footprint: 50% smaller installation area required

Operational Benefits:

Maintenance: Automated CIP reduces downtime by 70%
Scalability: Modular design enables easy capacity expansion
Integration: Compatible with renewable energy sources

INDUSTRIAL APPLICATIONS

Engineered solutions for demanding industrial environments

POWER GENERATION

Technical Requirements:

  • Cooling tower blowdown treatment
  • High TDS wastewater processing
  • Boiler makeup water recovery
  • Thermal discharge management

Challenges Solved:

  • Scale formation prevention
  • High temperature tolerance
  • Continuous operation requirements
  • Regulatory compliance assurance

TEXTILE MANUFACTURING

Technical Requirements:

  • Dye bath effluent treatment
  • Rinse water recovery systems
  • Chemical concentration management
  • Color removal processing

Challenges Solved:

  • Complex chemical composition
  • High color content removal
  • Variable flow rate handling
  • Strict discharge standards

PHARMACEUTICAL

Technical Requirements:

  • API manufacturing wastewater
  • Solvent recovery systems
  • Clean room discharge treatment
  • Validation documentation support

Challenges Solved:

  • GMP compliance requirements
  • Trace contaminant removal
  • Documentation & validation
  • Sterile processing needs

FOOD & BEVERAGE
Technical Requirements:

  • Process water treatment
  • CIP system effluent handling
  • Dairy wastewater processing
  • Sugar mill effluent treatment

Challenges Solved:

  • Food grade material requirements
  • High organic load processing
  • Sanitary design standards
  • HACCP compliance needs

TECHNOLOGY COMPARISON

Performance benchmarks vs traditional systems

PARAMETERTRADITIONAL MEEIONIC WATER HARVESTERIMPROVEMENT
Operating Temperature>150°C60-90°C60% Reduction
Energy ConsumptionHighLow60% Savings
Material ConstructionTitanium/DuplexFRP + Vinyl Ester40% Cost Reduction
FootprintLargeCompact50% Smaller
Maintenance FrequencyHighAutomated CIP70% Reduction
Water Recovery85-90%99%10-14% Higher

TECHNICAL FAQ

Engineering answers to common questions

Still have questions?

Contact our support team
The Water Harvester operates on the humidification-dehumidification (HDH) thermodynamic cycle. This process mimics natural evaporation and condensation, using low-grade thermal energy (60-90°C) to evaporate water from the waste stream, then condensing pure water vapor through efficient heat recovery systems. The multi-step energy recovery maximizes thermal efficiency while maintaining ambient pressure operation.
The system's FRP construction with Vinyl Ester Resin provides superior chemical resistance. The low-temperature operation prevents thermal degradation of complex compounds. The humidification process naturally separates dissolved solids while the multi-step concentration ensures maximum salt recovery. Advanced heat exchangers prevent scaling through controlled temperature profiles and automated cleaning cycles.
The system features IoT-enabled SCADA with real-time monitoring of temperature, flow, conductivity, and pH parameters. Automated Clean-in-Place (CIP) cycles are triggered by performance algorithms. Remote monitoring capabilities include predictive maintenance alerts, energy optimization algorithms, and integration with plant DCS systems. All safety interlocks meet international standards with redundant sensor systems.
The low-temperature operation (60-90°C) enables direct integration with solar thermal collectors, waste heat recovery systems, and biomass boilers. The system's thermal storage capability allows operation during variable renewable energy availability. Heat pump integration can utilize excess renewable electricity for thermal energy storage, making it ideal for sustainable manufacturing operations.

Technical Resources

Download detailed specifications and engineering data.

Zero Liquid Discharge

Zero Liquid Discharge

Our Clients

Trusted by Industry Leaders

Partnering with global organizations to deliver sustainable engineering excellence and innovative water and waste water treatment solutions.

  • Oil & Gas
  • Power & Utilities
  • Pharmaceuticals
  • Automotive & Engineering
  • Consumer Goods
  • Water Utilities
  • Reliance Industries
  • Dr. Reddy's
  • Coca-Cola
  • Indian Oil
  • Lupin
  • L'Oréal
  • Larsen & Toubro
  • Emcure
  • Bharat Petroleum
  • Samsung Engineering
  • SWCC
  • John Deere
  • Karnataka Power Corporation
  • Saudi Water Partnership Company
  • Tata Hitachi
  • Nilsan Nishotech
  • NTPC
  • Toyota
  • Aramco
  • BHEL
  • Mercedes-Benz
  • Dubai Electricity & Water Authority
  • ONGC
  • Bajaj
  • NPCIL
  • Tata
  • GAIL
  • Hindustan Petroleum
  • Marubeni
  • Tecton
  • Cumberland

Ready to Improve Your Process with Ionic?

Our team of experts is ready to help you find the most effective and innovative solution tailored to your specific requirements.

Get in touch with our experts

Have a custom requirement? Book a free consultation with our engineering team or drop us a message.

Contact Information

Call Us

020-27475272/73

020-29525874

+91 82754 86263

Mon-Sat, 9:30 AM to 6:30 PM

Visit HQ

S. No. 1, 5, 11-13, B Wing,
Mahalaxmi Heights, Mumbai-Pune Rd,
Pimpri, Pune-18, MH, INDIA.